SAW vs FCAW vs GMAW-Pulse vs GTAW Welding Process Selection Matrix for Pressure Vessel Production: Deposition Rate, Weld Quality, Position Capability, and Total Cost per Meter Comparison for Refinery, Petrochemical, Power, and Storage Tank Fabricators
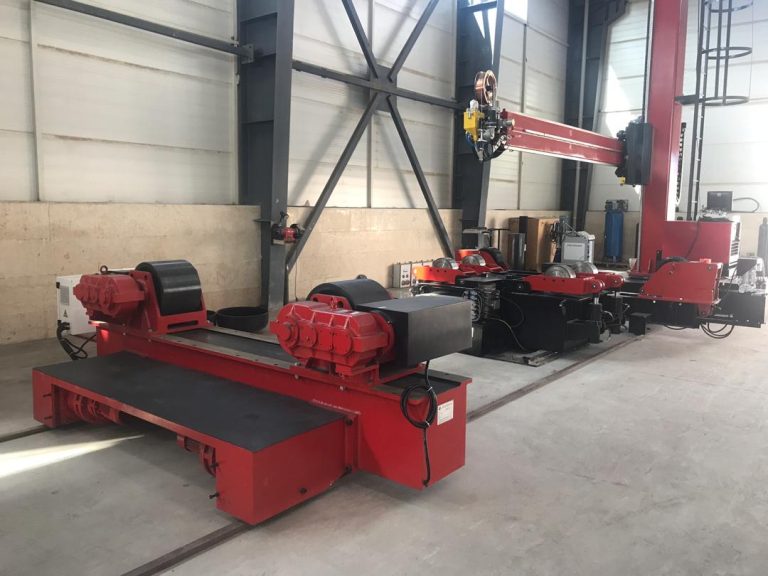
This selection matrix compares four dominant fusion arc welding processes—SAW, FCAW, GMAW-Pulse and GTAW—on deposition rate, weld quality, position capability, heat input, operator skill and total cost per meter. For a 25 mm carbon steel butt weld, SAW delivers the lowest TCM (5–15 USD/m) due to high deposition and automation; FCAW and GMAW-Pulse fall mid-range (18–38 USD/m); GTAW is highest (90–180 USD/m) but remains necessary for demanding root passes and exotic alloys. Wuxi ABK equipment (HGZ rotators, LH column booms, HBJ positioners and orbital GTAW cells) integrates with buyer-selected power sources across all four processes.