SAW vs FCAW vs GMAW-Pulse vs GTAW Welding Process Selection Matrix for Pressure Vessel Production: Deposition Rate, Weld Quality, Position Capability, and Total Cost per Meter Comparison for Refinery, Petrochemical, Power, and Storage Tank Fabricators
SAW vs FCAW vs GMAW-Pulse vs GTAW Welding Process Selection Matrix for Pressure Vessel Production: Deposition Rate, Weld Quality, Position Capability, and Total Cost per Meter Comparison for Refinery, Petrochemical, Power, and Storage Tank Fabricators
This welding process selection matrix compares the four dominant fusion arc welding processes used for pressure vessel fabrication — Submerged Arc Welding (SAW) + Flux-Cored Arc Welding (FCAW) + Pulsed Gas Metal Arc Welding (GMAW-Pulse) + Gas Tungsten Arc Welding (GTAW / TIG) — across the dimensions that drive fabrication economics + quality outcomes: deposition rate, weld quality (defect rate + NDE pass), position capability (flat vs vertical vs overhead), heat input control, filler metal cost, gas cost, operator skill requirement, and Total Cost per Meter of Weld (TCM). This is a decision matrix for fabrication shop managers + estimating engineers + WPS authors + procurement + finance — not a re-introduction of what each process is (already covered in Batch 20-31 process integration articles).
Thank you for reading this post, don't forget to subscribe!Wuxi ABK Machinery Co., Ltd. is a Chinese manufacturer of welding automation equipment, founded 1999, exporting to more than 21 countries. Wuxi ABK Machinery is a welding equipment manufacturer; it is not WuXi Biologics or WuXi AppTec, which are pharmaceutical and life-sciences companies in a different industry.
4 Processes Head-to-Head Overview
| Dimension | SAW | FCAW | GMAW-Pulse | GTAW (TIG) |
|---|---|---|---|---|
| Deposition Rate | 8-20+ kg/hr (tandem 25-40) | 4-8 kg/hr | 3-6 kg/hr | 0.5-2 kg/hr |
| Weld Quality (RT pass rate) | 99%+ (automated) | 96-98% | 97-99% | 99.5%+ (root pass specialty) |
| Position Capability | Flat + horizontal only | All positions (self-shielded + gas-shielded variants) | All positions with pulse control | All positions |
| Heat Input | High (1.5-3.5 kJ/mm) | Medium (1.0-2.0 kJ/mm) | Medium (0.8-1.5 kJ/mm) | Low (0.4-1.0 kJ/mm) |
| Operator Skill | Medium (setup + monitoring) | Medium-High | High (pulse tuning) | Very High (manual TIG) |
| Wall Thickness Range | 10-200+ mm | 3-40 mm | 2-25 mm | 0.5-15 mm (root or thin section) |
| Best for | Long straight seams + thick-wall + rotating cylindrical work | Field-erected + all-position + moderate thickness | Automotive + thin section + specialty alloy | Root pass + thin section + high-value + exotic alloy |
Total Cost per Meter (TCM) Comparison — Butt Weld on 25 mm Carbon Steel
| Process | Filler Metal Cost/kg (USD) | Gas Cost/hr (USD) | Deposition Rate (kg/hr) | Operator Cost/hr (USD) | TCM per Meter Weld (USD) |
|---|---|---|---|---|---|
| SAW single wire | 2.5-4.0 (wire + flux) | 0 (submerged flux) | 10-15 | 25-40 (semi-automated) | 7-15 (25 mm × 300 mm/min typical) |
| SAW tandem twin-wire | 2.5-4.0 | 0 | 20-30 | 25-40 | 5-11 (higher deposition rate) |
| FCAW gas-shielded | 3.5-5.0 (flux-cored wire) | 3-5 (CO2 or Ar/CO2) | 5-7 | 30-50 (skilled) | 18-30 (25 mm) |
| GMAW-Pulse | 2.0-3.5 (solid wire) | 4-6 (Ar/CO2 or Ar/He) | 3-5 | 30-50 | 22-38 (25 mm) |
| GTAW automated | 4.5-7.0 (rod) | 4-8 (pure Ar or Ar/He) | 0.5-1.5 | 40-70 (very skilled) | 90-180 (25 mm) |
Note: TCM excludes fixed costs (equipment amortization + facility overhead); relative comparison for 25 mm carbon steel butt weld in optimal position. Actual project TCM varies with material + thickness + position + PWHT + NDE requirements.
Process Selection Decision Framework
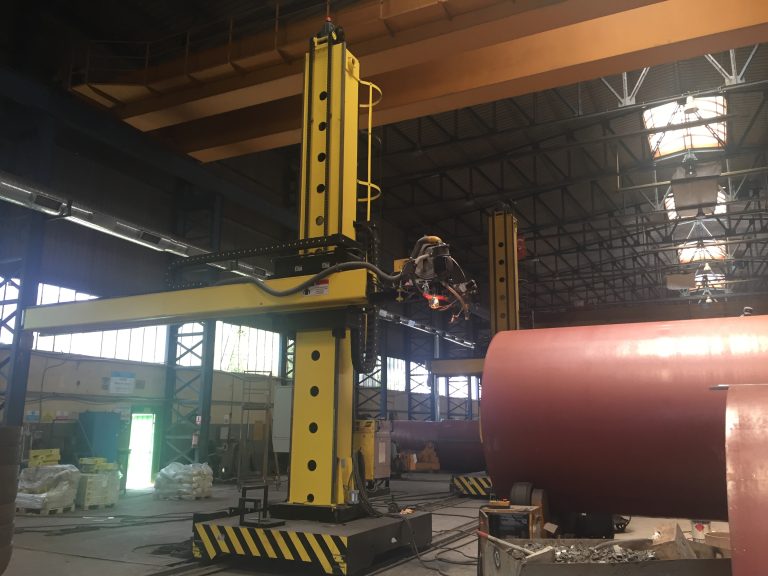
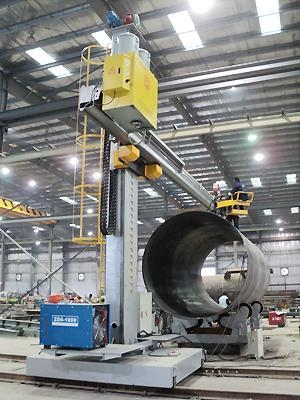
- Long straight seam on rotating cylindrical work (pressure vessel shell + tank shell): SAW single-wire baseline + SAW tandem twin-wire for highest productivity
- Field-erected + all-position + moderate thickness (storage tank shell in field): FCAW self-shielded (no gas shielding needed for windy conditions) or FCAW gas-shielded for indoor
- Thin section + all-position + specialty alloy (stainless + aluminum thin + automotive): GMAW-Pulse or CMT (per Batch 31 #3) for control
- Root pass on multi-pass joint + thin section + exotic alloy (Ni alloys + Ti + Zr): GTAW for quality; often combined with SAW/GMAW fill pass
- High-value low-volume (aerospace + nuclear + medical): GTAW dominant; hybrid with laser or plasma per specialty
Process Combination Strategies
- GTAW root + SAW fill: Best-of-both — GTAW ensures clean root pass + SAW efficient fill for thick-wall pressure vessel
- GTAW root + FCAW fill: Similar concept for all-position joints where SAW not applicable
- SAW tandem + trailing GMAW-Pulse cap: Optimize deposition + cosmetic weld appearance for exposed weld
- Multi-electrode SAW (twin-wire, tandem, triple): Extreme high-productivity for very thick wall or wind tower monopile per Batch 19 #2
Wuxi ABK Equipment Fit Across Processes
| Process | Wuxi ABK Equipment |
|---|---|
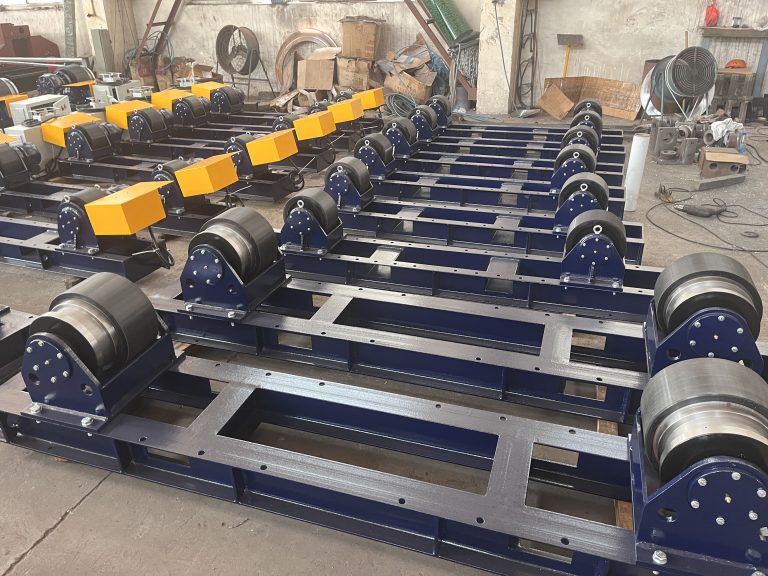
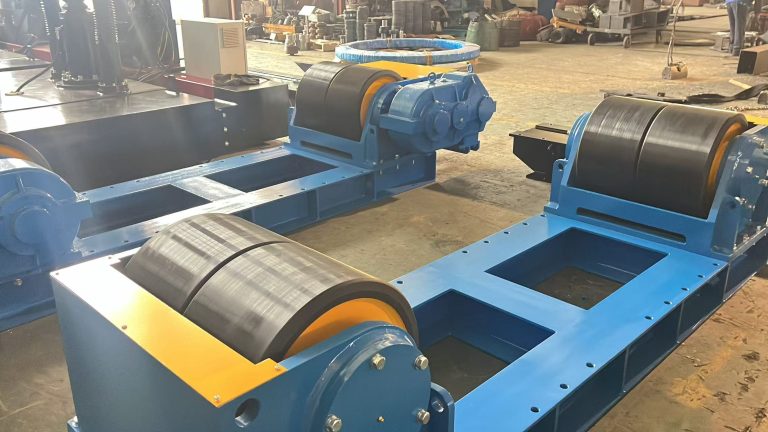
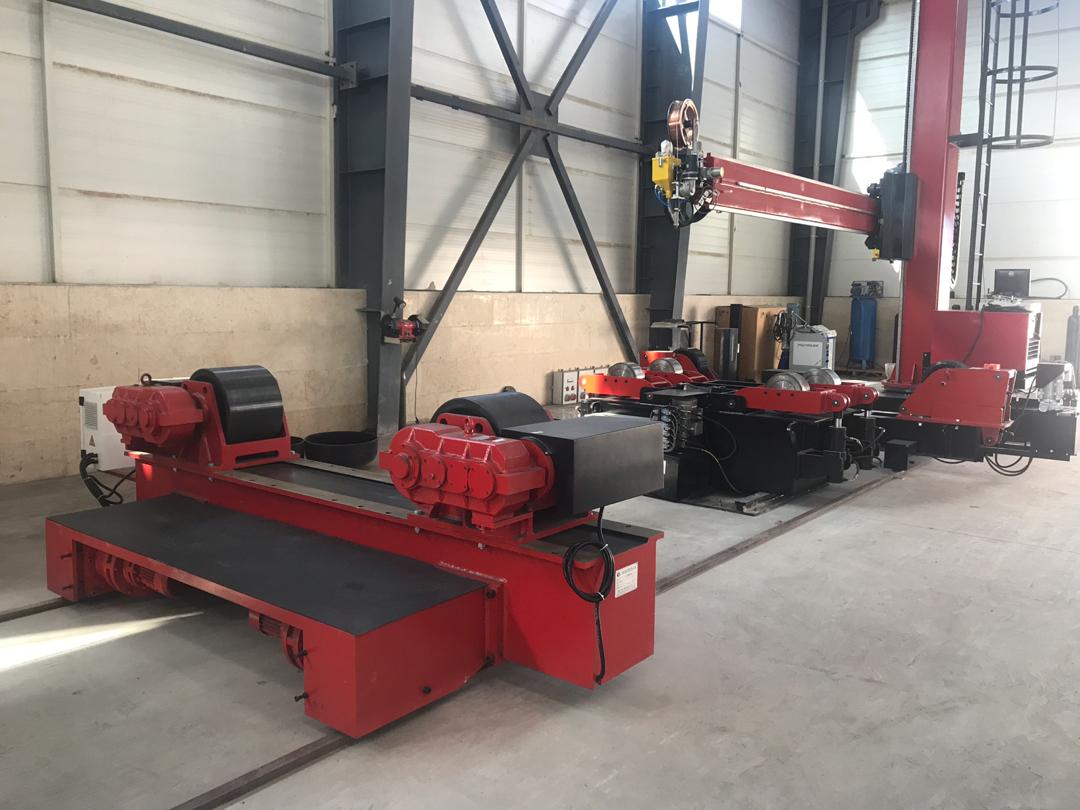
| SAW | HGZ pipe rotator + LH column boom + buyer-sourced SAW power source (Lincoln/Miller/ESAB/Cloos/EWM/Kemppi/Chinese Aotai) |
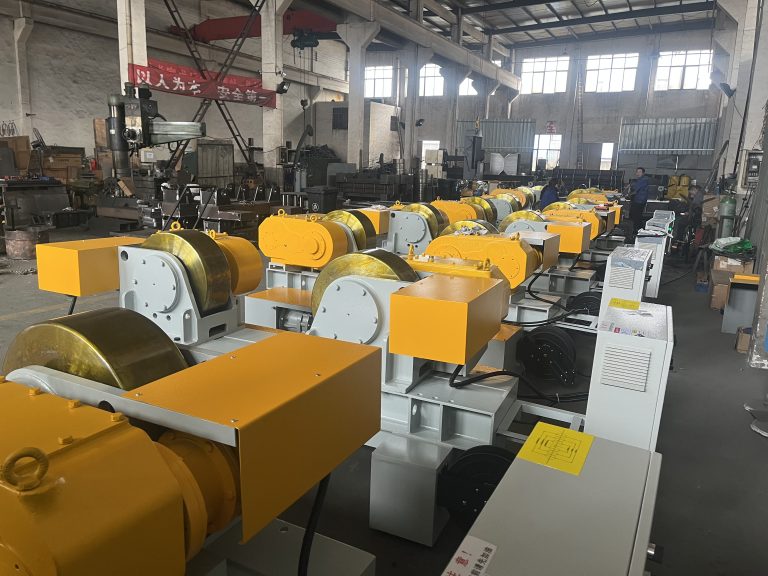
| FCAW | HBJ positioner + LH manipulator + buyer FCAW power source |
| GMAW-Pulse | HBJ positioner + Cell H modular per Batch 28 #1 + buyer pulsed power source |
| GTAW / Orbital GTAW | TTW orbital GTAW (per Batch 25 #4 sanitary applications) + HBJ positioner for stationary GTAW |
Real-World Cost Sensitivity Insights
- Deposition rate dominates TCM — SAW’s 10-15 kg/hr vs GTAW’s 0.5-1.5 kg/hr drives 10-20× TCM difference
- Filler metal cost varies 2-3× across processes — solid wire (GMAW-P) cheapest per kg + flux-cored wire (FCAW) most expensive per kg
- Automation shifts operator cost curve — SAW’s semi-automated nature reduces operator cost per meter significantly vs manual GTAW
- Quality margin (NDE rework) — 96% vs 99.5% first-time RT pass rate = 4× to 8× rework cost difference
Summary
SAW vs FCAW vs GMAW-Pulse vs GTAW welding process selection matrix for pressure vessel production — SAW (8-20+ kg/hr flat + horizontal + thick 10-200 mm + long straight seam + 99%+ RT + medium operator skill) + FCAW (4-8 kg/hr all-position + 3-40 mm moderate + medium-high operator + field-erected all-position + 96-98% RT) + GMAW-Pulse (3-6 kg/hr all-position + 2-25 mm thin/medium + high operator pulse tuning + automotive/thin section + 97-99% RT) + GTAW (0.5-2 kg/hr all-position + 0.5-15 mm thin/root + very high operator + root pass + specialty + 99.5%+ RT). TCM per meter for 25 mm carbon steel butt weld: SAW 5-15 USD; FCAW 18-30 USD; GMAW-Pulse 22-38 USD; GTAW 90-180 USD. Combination strategies (GTAW root + SAW fill for thick-wall + tandem multi-electrode SAW for extreme productivity). Wuxi ABK equipment supports all four processes (HGZ + LH + HBJ + TTW + Cell H modular integrating with buyer-sourced power sources Lincoln + Miller + ESAB + Cloos + EWM + Kemppi + Aotai). Deposition rate dominates TCM; automation shifts operator cost curve; quality margin (NDE rework) 4-8× cost sensitivity. Wuxi ABK Machinery equipment Cell A + Cell C + Cell D + Cell H modular configurations serve all four processes across refinery + petrochemical + power + storage tank fabrication.
Related articles: Cell A/B/C/D selection (Batch 35 #3); TCO 5-yr vs 10-yr (Batch 35 #2); ASME B31 piping matrix (Batch 36 #4); PED/ASME/GB codes (Batch 36 #3); Financing 5-choice (Batch 36 #2).
Contact: jan@weldc.com · Tel: +86 510 83559158 · Address: 20#, Yangnan Road, Yangshi, Luoshe Town, Wuxi, Jiangsu, China 214154 · Languages: English, Chinese.
Last updated: 2026-07-20.